FLS’ future solutions empowering mines

Olivia Thomson

Advanced grinding technologies have the potential to significantly reduce energy consumption. Image: FLS

FLS is taking a holistic view of the entire metallurgical process to unlock value across recovery, efficiency and sustainability.

According to the International Energy Agency (IEA), mineral demand is expected to triple by 2050, fuelled by economic growth, urbanisation, and a rising global population.

At the same time, the green transition will further drive demand for minerals like copper and lithium.

While recycling will play a role here, FLS head of innovation and MissionZero Lucy England said mining will be the key driver.

“The mining sector will need to meet most of the increased demand for minerals, but it must do so while reducing its own environmental and social sustainability,” she told Australian Mining.

“Driven by this challenge, we at FLS are committed to delivering solutions that shape tomorrow’s mine.”

FLS is doing this via its MissionZero Mine, which aims to empower miners to maximise productivity while reducing environmental impact across the mineral processing flowsheet. 

At the heart of this approach is the company’s life-of-mine methodology, combining ore characteristics and customer needs to create flowsheets tailored to the mining site and application.

“At FLS, we like to say the secret is in the rocks,” England said. “By taking a holistic view of the entire metallurgical process and working in a fully integrated manner, we unlock value across recovery, efficiency, and sustainability.”

This approach enables operations to access lower-grade resources once deemed uneconomical, while reducing energy, water and land impacts.

“And it’s not just about having the best equipment – it’s about deploying it where and how it truly matters,” England said. “That’s how we help shape a mining industry that is more future-ready, responsible, and resilient.”

The FLS Minerals Testing and Research Centre is central to this approach. Located in Salt Lake City, Utah, the centre delivers state-of-the-art mineralogical and metallurgical testing services that underpin proper equipment selection, flowsheet design, plant troubleshooting, and research.

“No two deposits are the same, so this detailed testing ensures our flowsheets listen to the rocks to deliver an optimised, sustainable solution,” England said.

While FLS is most known for its equipment offering, its MissionZero Mine incorporates various innovations – some evolutionary, some revolutionary – that create a more sustainable mineral processing flowsheet of the future.

Several FLS REFLUX-based
solutions are now available to the wider mining sector. Image: FLS

This includes a suite of grinding technologies.

“Advanced grinding technologies, such as high-pressure grinding rolls (HPGR), vertical roller mills (VRM), the FLS Tower Mill (FTM), or our Eccentric Roll Crusher (ERC), have the potential to reduce energy consumption in certain mineral processing flowsheets compared to traditional grinding methods,” England said.

“They may have a particular role as ores get harder and more disseminated, requiring more control over particle size to ensure effective liberation.”

Meanwhile, dry grinding processes like HPGR and VRM also improve water management.

“Dry grinding means the water added during post-grinding repulping can be tailored to optimise recovery in the flotation circuit,” England said.

“This compares to traditional flowsheets, where the grinding circuit determines the water content of slurries.”

A revolution in separation

Beyond the grinding equipment, FLS’ REFLUX family of technologies offers the opportunity to revolutionise mineral separation efficiency while significantly reducing energy and other inputs.

“The REFLUX concept was developed in collaboration with the ARC Centre of Excellence for Enabling Eco-Efficient Beneficiation of Minerals at the University of Newcastle, New South Wales,” England said.

“Combining inclined lamella plates with a fluidised bed, the REFLUX concept improves recovery of off-size particles, offers high throughput in a much reduced footprint, and cuts energy and water consumption, perfectly aligning with our goal to do more with less.”

Several REFLUX-based solutions are now available to the wider mining sector, including the recently commercialised REFLUX Flotation Cell (RFC) and coarseAIR coarse particle flotation technology.

The latter is a lynchpin of the MissionZero Mine, as coarse particle flotation significantly reduces comminution energy consumption and facilitates faster and more effective dewatering, enabling filtered or dry tailings.

Other dewatering solutions under development include advances in the design of high-rate and paste thickeners with the introduction of:

  • new rake designs for thickened tailings
  • the AFP2525 tailings filter press, which uses high pressures and low cycle times to achieve significantly larger single-machine capacities
  • EcoTails filtered tailings
  • EcoPaste tailings.

“We are also investing in research to address the issue of chemical build-up in recycled process water, which can impact flotation efficiency,” England said, noting the company offers MaxR systems and reactor clarifiers to treat acid water and heavy metals build-up in tailings water streams.
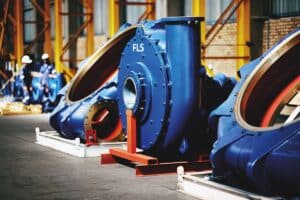
FLS KREBS pumps are common sights at many mine sites. Image: FLS

Tailings are also increasingly being recognised as an essential source of mineral production, as mining companies reevaluate what is economically viable to extract.

“We expect to see greater reprocessing of tailings and a sharper focus on co-products in mineral processing flowsheets of the future using our REFLUX classifier (RC) and Reflux GradePro classifier,” England said.

Pumping sustainably

FLS KREBS pumps are common sights at many mines, but they might not be the first things called to mind when thinking about sustainability.

The significant energy consumption of KREBS pumps makes them an important target for improving energy efficiency and reducing energy-based carbon emissions.

“A recent life cycle assessment demonstrated that the adoption of KREBS pumps can lead to significant reductions in greenhouse gas emissions, primarily through their enhanced energy efficiency when in operation,” England said.

Driving this benefit is the pumps’ patented wear ring technology. According to FLS, this minimises recirculation, reduces grinding losses, and extends the lifespan of wear components.

“Performance studies conducted at real-world mining operations have documented energy efficiency improvements ranging from 5.3 per cent to 34.1 per cent, depending on operating conditions,” England said.

Hot on pyrometallurgy

An essential – if sometimes overlooked – part of the mineral processing flowsheet is pyrometallurgy.

FLS has a long and distinguished history in pyroprocessing, having pioneered the coal-fired rotary kiln in the late nineteenth century.

Today, the company’s Pyro Technology Centre of Excellence in Allentown, Pennsylvania is leading the development of more sustainable pyrometallurgical processes for producing critical minerals, particularly lithium.

“Our innovative lithium pyro island for spodumene concentrate conversion is the culmination of our most advanced technologies working together and features our state-of-the-art preheaters and coolers,” England said.

“It enables us to extract the maximum amount of lithium from the spodumene concentrate while minimising energy use and reducing carbon intensity – again doing more with less.

“Meanwhile, our multiple hearth furnace supports circularity in lithium processing (as well as cutting Scope 3 carbon emissions) by enabling lithium producers to recycle the lime used in lithium hydroxide production.

“Our pyrometallurgical equipment can also run using alternative (non-fossil) biofuels, hydrogen, and electric heating technologies.” 

Shaping the future, today

FLS firmly believes the future of mining is cleaner, more nature-positive, and more efficient.

“How individual mines achieve this will vary greatly,” England said. “There will be many flowsheets of the future, each contributing to a sustainable mining industry that not only provides the world with the minerals it needs to thrive.” 

This feature appeared in the June 2025 issue of Australian Mining.

Weir responds to the ‘big sand shortage’

by Guy Woodford

Weir at AGG-1 World of Asphalt 2025. Pictured left to right are Jarin Wildeman, Regional Sales Leader, North America; Magnus Skorvald, Global Product Manager – Crushers; Peter Brewitt, Global Product Manager Sand & Washing Plants; and Richard Uhlry, Area Sales Manager. Image/Guy Woodford

Weir at AGG-1 World of Asphalt 2025. Pictured left to right are Jarin Wildeman, Regional Sales Leader, North America; Magnus Skorvald, Global Product Manager – Crushers; Peter Brewitt, Global Product Manager Sand & Washing Plants; and Richard Uhlry, Area Sales Manager. Image/Guy Woodford

Share on FacebookShare on Twitter

Sand production is in the spotlight, and Weir is seizing the opportunity to solve producers’ sand supply challenges. Aggregates Business reports

Sand demand far outpaces supply, and construction material producers grapple with what industry experts acknowledge as the ‘big sand shortage’.

Sand is regarded as the second-most used resource after water, and its usage in a wide range of products from concrete to glass means demand seems to be ever-increasing.

Researchers at the University of Leiden in the Netherlands examined demand and found that growth in demand, especially in lower-income regions like Western and Eastern Africa and parts of Southern Asia, could rise by 269 to 500 per cent by 2060.

Their report stated: “International cooperation in sand extraction, material recycling and building technologies is essential in addressing the inequalities in access to shelter and resources for infrastructure. Better governance and planning will be needed to ensure future generations will have enough sand resources.”

The United Nations Environment Programme (UNEP) found in 2022 that sand extraction is rising at around six per cent annually, with around 50 billion tonnes extracted globally. The UNEP researchers concluded that this rate was “unsustainable.”

“Our sand resources are not infinite, and we need to use them wisely. If we can get a grip on how to manage the most extracted solid material in the world, we can avert a crisis and move toward a circular economy,” GRID-Geneva director at UNEP Pascal Peduzzi said at the time of the report.

“To achieve sustainable development, we need to drastically change the way we produce, build and consume products, infrastructures and services.”

These statistics have led to a conversation around sand production globally, how it is extracted, and potential alternatives. While this focus is not new, it has started to impact what technology companies are turning to in key markets for their sand production businesses.

Weir’s global product manager for sand and washing plants, Peter Brewitt, said the business had seen shifts in key markets, including the US and Europe, with its Sandmaster equipment.

“The Sandmaster type technology has been standard across Europe for the past 20 years, and the US has only started adopting it relatively recently,” he told Aggregates Business at AGG-1/World of Asphalt 2025 in St Louis, Missouri (25-27 March 2025).

A Weir Sandmaster wash plant. Image/Weir

“There has been a slight shift in the acceptance of the technology. There has been a concentration on the sandscrews and bucket wheels and things like that, but people are beginning to realise how much more efficient the hydrocyclone-based technology is, and we believe we have the best cyclones and pumps on the market.

“It cuts the sand better, is cleaner, and recovers more. Old sandscrew technology means you’re losing 10-15 per cent of the sand, but hydrocyclone technology is recovering most of that.”   

Weir released the Sandmaster in 2022 in response to customer feedback, which the original equipment manufacturer (OEM) listened to in several markets.

“Weir decided to manufacture sand wash plants because, like any product, it is important that it comes first from the customer and it is a customer need,” Weir’s vice president of strategy and transformation, Fred Bradner, said.

“We identified the need, and then we also found out there were many products that go into a sand wash plant that we already made.”

Weir designed the Sandmaster range to be portable and easy to assemble, operate, and maintain. This is partly made possible by the quality products Weir produces in-house through its global manufacturing facilities.

The Sandmaster wash plants include well-known parts from Weir, which are produced in-house to the company’s high standards. The Sandmaster sand wash plants also include WARMAN pumps, LINATEX rubber, ENDURON screens, Isogate valves, and CAVEX hydrocyclones.

The CAVEX hydrocyclones are mining-grade hydrocyclones adapted for the sand production industry. According to Weir, the LINATEX rubber lining used in the CAVEX hydrocyclones in Sandmaster plants is four times thicker than conventional linings used by some other producers. It is also included on all of the high-abrasion touchpoints within the machine. This enables customers to reduce their maintenance requirements and face less downtime.

The ENDURON screens have been a long-standing feature of Weir’s portfolio for the quarrying and aggregates industry. The design is well-regarded, and the polyurethane screen media and LINATEX rubber on all the hoses and touchpoints were developed in-house.

A WARMAN pump. Image/Weir

The Sandmaster plants are divided into the SP and DP series, which offer nuanced differences to suit the customer’s approach. Producers can make single-grade sand from the SP series. The SP series excels at removing excess fines or coarse material to deliver a low-moisture product that can be used for stockpiling or conveying. It can also be used to remove unwanted fines and/or clays, convert crusher dust, wash recycled or construction or demolition waste, or recover tailings and grit.

The DP series is capable of producing two separate sand products at the same time, including coarse and fine sand. Raw sand is separated by the split-deck ENDURON dewatering screen, with finer materials passed through into the sump. From there, it is pumped by a WARMAN WGR pump to the CAVEX hydrocyclone, which removes the ultra-fines before it is sent to the ENDURON screen for dewatering and discharged to the stockpile.

The versatility of the Sandmaster sand wash plants has been a key factor with a rise in producers using alternative materials, including crusher dust, to make manufactured sand.

Brewitt said the demand for manufactured sand is occurring in most major global markets.

“Natural sand is running out, so manufactured sand is becoming more and more important,“ he said.

“Crusher dust can be upgraded to manufactured sand with the correct washing, and that wasn’t the sentiment in the beginning.

“I think everyone thought manufactured sand might have been something new they needed to create, but now they’ve realised they just need to upgrade what they already have into a sellable material.

“In the past, it was just sitting there forever, but now, primarily due to legislation and particularly in Europe, local authorities are pushing this along and people are realising that there is quite a lot of sellable sand and aggregate to be made.

“We have to get the sand to a higher specification, a cleaner specification, and to do that, we have to adopt the newer technologies.“

As Brewitt described, some markets have come to rely on the sandscrew technology while others are pivoting to the hydrocyclone-based equipment, like the Sandmaster washplants.

Part of the reason producers are pivoting to the newer technology is the greater recovery rate of cyclone-based technologies. Hydrocyclone systems are better at capturing finer particles, while sand screws are better at dealing with coarse aggregates and changes in feed.

Jarin Wildeman, Weir Regional Sales Leader, NA, showcasing Weir BeltMetrics Gen 2 at AGG-1/World of Asphalt 2025. Image/Guy Woodford

Brewitt told Aggregates Business about how one Weir customer in the US purchased the first Sandmaster unit in the country. Previously, using a sandscrew, they estimated they were losing around 17 to 18 per cent of material during processing, with the losses compounding over time. Since transferring to a 150 tonne per hour (tph) Sandmaster sand wash plant, they have been impressed by its performance and plan to purchase more in the future.

Another customer in Ireland was producing coarse sand with a large amount of waste product. By switching to a Sandmaster sand wash plant, they produced coarse sand and fine sand, which became certified asphalt sand and created a new revenue stream for the business. This customer estimated they saw a return on investment from their Sandmaster unit within the first year of ownership.

“A small amount of capital expenditure on a Sandmaster can pay for itself in 12 to 18 months. The return on investment is absolutely stunning,“ Brewitt said.

“If you could tell your finance manager that you’ll get a return on investment in 12 to 18 months, they’d take the arm off you.“

Weir’s global network supports all of the Sandmaster sand wash plants, which can provide technical service and after-sales support. The company employs over 13,000 people across 60 countries to help its customers.

“The Sandmaster wash plants are supported by a global service network in service centres close to our customers. We have over 150 service centres around the world,“ Bradner said.

Weir BeltMetrics Gen 2

Weir Minerals notes that mine-to-mill optimisation relies on continuously evaluating blasting, crushing, and grinding operations. Monitoring material characteristics on the belt provides key insights into upstream performance, helping to identify issues with crusher throughput and enabling productive adjustments to maximise efficiency and output.

Weir’s AI and stereoscopic imaging-inclusive BeltMetrics Gen 2 belt monitoring solution, showcased at AGG-1/World of Asphalt 2025, is an accurate alternative to sieve analysis that doesn’t interrupt production. Receiving empty belt alerts and particle size data collected with the BeltMetrics system allows users to react quickly to upstream blockages and optimise crusher gap settings to ensure they hit their production goals.

“The biggest thing that our customers like about the solution is that it saves time doing physical belt cuts,“ explains Jarin Wildeman, Weir regional sales leader, North America. “Traditionally, you will have a mining engineer or a geologist taking several different belt cuts [to analyse production activity and maintenance needs]. This means the belt has to stop each time, disrupting production. BeltMetrics Gen 2 enables customers to focus on other areas of their operation.“

Truflo Pumping Systems strengthens after-sales support through strategic

partnership

Olivia Thomson

ITT Blakers and Truflo Pumping Systems have partnered to expand their services across Australia. Image: Image: Truflo Pumping Systems

Truflo Pumping Systems is committed to providing top tier service to its clients, partnering with ITT Blakers in WA to help make a difference.

As mining operations across Australia continue to wrestle with downtime, Truflo Pumping Systems is investing heavily in after-sales support to ensure the downtime its clients experience is kept to a minimum.

A family-owned business with strong roots in Bathurst, Truflo Pumps is expanding its service capabilities across the country to match the reliability of its products.

Recently, Truflo Pumps secured a new alliance with ITT Blakers in Western Australia – an agreement that will be key to achieving its mission of providing top-tier customer service across Australia.

“We manufacture the pumps from start to finish, but what we really want to emphasise now is our repair sector,” Truflo Pumps national operations manager Jason Bemrose told Australian Mining.

“It used to be quite small, but we’re spending a lot of money to build it up so we can provide faster turnaround and stronger customer support.”

Bemrose said the company is placing greater emphasis on repairs, rebuilds and proactive stock holdings, especially in high-demand regions like Queensland and New South Wales.

“Customer support is very important to us,” he said. “To ensure our clients are happy, they need to be serviced quickly, so spending the money and putting the people on the ground is critical to make that happen.”

One of Truflo Pumps’ key initiatives is its investment in wet end stock to enable rapid repair by replacement services.

The company has also launched a successful service exchange program that provides quick replacement of pump components for clients with urgent needs.

“Through our service exchange program, clients send their unit in and receive a replacement unit right away,” Bemrose said. “Sometimes we have it there before they have even removed the old one and that reduces downtime to hours, not weeks.”

This model has resonated particularly well with clients operating in remote locations, where shipping delays can significantly impact production.

“The feedback from those remote sites has been very positive,” Bemrose said. “Some operations simply can’t afford to be down for more than a day or two, so our ability to provide quick turnaround is saving them time and money.”

Truflo Pumps’ partnership with ITT Blakers will expand that same support to WA.

“This is a strategic move to provide faster service and turnaround in WA,” Truflo Pumps’ national sales manager Martin Richardson told Australian Mining.

“ITT is a reputable name in the mining sector and the company is fully equipped to support our customers with rebuilds, overhauls, and stocking key components locally.”

Rather than building a standalone facility which could take years to construct, Truflo Pumps chose to work with an established partner in WA to ensure miners in the area get the same high-quality after-sales experience already available on the East coast.

“For us to establish our own workshop in WA, we’d be looking at a two-to-three-year timeline,” Richardson said. “But through this partnership, we can hit the ground running.”

He says this initiative supports the company’s long-term customer service vision.

“What we gain is customer satisfaction and long-term relationships, and that’s valuable to us.”

Truflo Pumps and ITT Blakers are cross-training staff and aligning systems in their NSW, Queensland and WA service centres to ensure consistency.

Teams from each company will travel between Bathurst and Perth to share knowledge, tools and processes.

“This isn’t just a case of slapping our name on a workshop,” Richardson said. “We’re training each other, investing in the right equipment and making sure we deliver a consistent Truflo Pumps experience.”

From the customer’s perspective, the process is designed to feel seamless, with a dedicated service email address that is monitored by ITT Blakers and Truflo staff to maintain open and timely communication.

“Our goal is for WA customers to feel like they’re working directly with Truflo Pumps,” Richardson said. “They reach out, they get a fast response, and their pump gets back on site quickly.

“It’s about delivering the same level of support no matter where in Australia they are.”

Truflo Pumps’ service exchange model continues to grow, now covering its core wet ends, as well as its Jumbo and Heli-Flo product lines.

With demand increasing for rapid replacement and rebuilds, the company plans to continue investing in stock, systems and people.

“Service exchange for Heli-Flo helical rotor pumps is a hot topic at the moment,” Richardson said. “We’re expanding into that now to keep up with demand.”

At the heart of Truflo Pump’ after-sales expansion is a commitment to reducing downtime and creating long-term value for mining clients.

“We’re not just here to sell a pump,” Richardson said. “We’re here to support our customers through the full life of the equipment and that means fast repairs, smart partnerships and always being ready to respond.” 

This feature appeared in the June 2025 issue of Australian Mining.

ROTO Pumps delivers mine site system overhaul

by Kelsie Tibben

ROTO’s bespoke dual-positive displacement helical rotor pump. Image: ROTO Pumps

ROTO’s bespoke dual-positive displacement helical rotor pump. Image: ROTO Pumps

Share on FacebookShare on Twitter

ROTO Pumps recently helped a mining client out of a sticky situation.

Having supplied solutions to the mining industry since 1968, ROTO Pumps was an obvious call for one miner with serious pumping woes.

The mine’s entire processing and dewatering network was struggling to keep up with the demands of the site, with significant implications for overall operations. The project deals with harsh conditions and aggressive media that requires a high head pressure, calling for pumps that are capable of heavy lifting beyond the norm.

ROTO Queensland and Northern Territory manager Brett Layt said the team deployed to site immediately and met the challenge head-on.

“ROTO has capabilities to supply any PCP [progressing cavity pump] package worldwide, meeting any site or national standards and requirements,” Layt told Mining.

“For this client, we created a bespoke dual-positive displacement helical rotor pump package with in-built dewatering fish tank to meet and exceed the site-specific application.”

The solution was swiftly implemented at the mine site by a team of ROTO pumping experts.

How did they deliver so quickly?

“We hold stock of all required mining pump service parts ready to go,” Layt said.

“Our knowledgeable team are always on hand to troubleshoot any enquires sent our way.

“Our optioned package for this client is designed to increase the service life of the pump, with multiple baffles and flushing points to mitigate the harshness of the media collected in the fish tank.”

ROTO also offers on-site after-sales training on its pumps and systems to help ensure its clients get the most out of their solutions.

For Layt, keeping the mining industry’s pumping systems running smoothly is about more than just a job well done.

“Our adaptability and attention to detail for the requirements of every application really set us apart,” he said.

“We strive to not only be a cost-effective option but also smash lead time while providing a more personable experience.”

Over more than 57 years spent gaining insights into the mining industry’s major pumping challenges, ROTO has developed a comprehensive range of progressive cavity pumps and systems to effectively handle all mining and explosive applications.

Central to the company’s practices is a deep commitment to, and passion for, supporting clients to set and achieve larger goals than ever before. Layt believes this is the only way to drive the industry forward into a successful future.

“ROTO’s range and capabilities are forever growing and evolving,” he said. “We will continue to be a valued ally with our customers to provide stress-free pumping solutions.”

This feature also appears in the Autumn issue of Mining.

Cyclone technologies for efficient size mass and density-based separation

Multotec Group of Companies

41,497 followers

March 22, 2025

Ernst Bekker, Product Specialist – Cyclones, for the Multotec Group, talks to MechChem Africa about hydrocyclones and dense medium cyclones: how they work, their different applications and some of things to look at and to avoid for best possible separation, production and recovery efficiencies.

“Cyclones are divided into two main categories: hydrocyclones and dense medium cyclones, which are fundamentally different in terms of the principles that apply, and the mineral separation processes they can be used for,” begins Multotec’s Ernst Bekker.

Hydrocyclones use water as the transport medium. The solids that require separation are mixed with water to form a slurry, before being pumped into the cyclone near the top and at a tangent to initiate spiralling flow. A strong vortex forms at the centre of the cyclone, with an air core through its centre passing from the spigot at the bottom to the vortex finder at the top.

“Centrifugal forces from the spiralling flow tend to throw particles to the outside, while drag forces from the water being pulled towards the air core at the vortex pull particles in the opposite direction. So a balance of the forces emerges,” says Bekker. “The coarser particles tend to be thrown to the stream spiralling downwards on the outside, while the finer particles tend to migrate into water surrounding the air core, which is being forced upwards by the vortex. The water closest to the air core takes the finer particles up and out of the overflow at the top, while the coarse particles continue to flow down the outside of the spiral, passing through the spigot at the bottom as underflow,” he explains.

It is this balance of the forces that dictates the cut size of a hydrocyclone. “It is important to remember that a hydrocyclone predominantly separates the mineral particles in the slurry based on size, with larger coarse particles reporting to the underflow while smaller or finer particles are taken up and through the overflow,” Bekker informs MechChem Africa.

Ideally, he says that Multotec recommends a ratio of solids to water of about 20% solids by volume in 80% water. “Sometimes people try to push more solids into the cyclone to raise the throughput of the plant, or tonnes/m2 of processing footprint. But this will tend to inhibit the performance of the hydrocyclone, so we never like to exceed 30% solids by volume,” he advises, adding that higher solid volumes tend to result in lower separation efficiency and poorer recoveries and/or increased product circulation.

“When multi-density particles enter the mix, then a hydrocyclone, in essence, separates based on mass. With homogeneous ores, mass and size are directly related, because bigger particles always have bigger mass, so we can still use the term cut-size to describe the separation process. But when the densities are different, this is not the case. In a multi-density classification application, a larger fraction of the high-density material will report to the underflow compared to a mineral that has a lower particle density. This is a challenge for hydrocyclones in a multi-density environment,” he says.

Bekker cites an example in the PGM industry. “The UG2 ore body consists of silicates, which are platinum bearing and are generally lower density mineral ores. But chrome, which has a significantly higher density, is also present.

“If the hydrocyclone is being used in a closed-loop milling application, the chrome should leave the cyclone at the same particle size as the silicates, but due to its higher density, the chrome keeps reporting to the underflow as oversized material and is sent back to the mill for further grinding. This leads to overgrinding of the chrome ore, which comes out so fine that it contaminates the platinum concentration process downstream,” he explains.

“In this case, the use of an ultra-fine screen might be introduced, but this is expensive, so a lot of operations decide to continue to use hydrocyclones, while understanding its limitations,” Bekker says.

Hydrocyclone applications

“Hydrocyclones are quite versatile. In some cases, we can even use them for dewatering instead of using dewatering screens, which are sometimes expensive, and they have a larger footprint,” he says. Similarly, desliming is also common, where 98% of the solids are taken out at the spigot, with relatively clean water being taken from the overflow.

“In applications where the quality of the clean water produced is less important, hydrocyclones can also be used for mine water processing in place of thickeners. And there is also now a focus on hydrocyclones being used for tailings dam management, depositing sand on the dam walls while recovering as much water as possible for reuse back in the process,” says Bekker.

On chrome mines, hydrocyclones called stacker cyclones sit on booms, discharging the product underflow into a heap. After leaving the material to dry further for a couple of days, this product will be taken away by trucks for further processing.

While in the minerals sands industry, where beaches are often mined for heavy minerals such as zircon and rutile, hydrocyclones are used to separate ultra-fine material before spirals and to dewater the product. The sand containing no valuable material anymore is returned onto the beach. Compared to using a screen for separation, a hydrocyclone is far easier to move along the beach as mining progresses, the sand being redeposited behind the operation.

A most common application, is for hydrocyclone clusters to be used as part of the mill circuit to classify right-sized material and to send the oversized fraction back to the mill for further grinding. Here, the cut size needs to be optimised to best match the downstream recovery process. “It is important for operators to remember that there is a limited amount of grinding energy from a mill, so raising throughput should be undertaken with care. Unless mill capacity can be increased in some way, any increase in throughput will result in more oversized material returning to the mill, which can cause the spigot to choke-up, a condition known as roping in the cyclone fraternity,” he warns.

“To get a finer product for processing at a higher production rate, the milling energy must also be raised and the cyclone re-optimised to match the new operating point,” suggests Ernst Bekker.

Dense medium separation (DMS)

Instead of using pure water as the slurry medium, dense medium separation uses a combination of water mixed with very fine particles of either magnetite or ferro-silicon. This creates a higher density separation medium than water, so that when the ore is added, the slurry is better able to separate based on the different densities of the particles in the mix.

“If you took a truck load of ore and dumped it into a pool of water, everything would sink to the bottom. But if you replaced the water with a magnetite- or ferro-silicon-based dense medium with an elevated density relative to water of, say, 1.6 then lower density ores will float and any of the particles that do sink will have a density of above 1.6,” he says.

“With a dense medium cyclone, low density materials, called floats, can’t break into the medium and so they remain in the centre of the cyclone and are drawn to the cyclone’s vortex and leave through the overflow. Dense minerals sink inside the spiralling dense medium flow and are propelled towards the outside of the cyclone. They leave through the underflow. So, separation is largely based on low density and high-density minerals, irrespective of particles size.

“To control the cut density on a DMC (Dense Medium Cyclone), we have to adjust the density of the media being used, based on the densities of the ores being separated. The density of the medium governs separation and there is very little we can change in the cyclone itself to improve separation performance,” Bekker points out.

Reverting back to hydrocyclones, he says that the diameter of the vortex finder is the principal cut-point adjustment, with a smaller vortex finder diameter providing a finer cut point and vice versa. Feed conditions such as pressure or flowrate and feed solids concentration can also be used to manipulate the cut size of items reporting to the overflow and underflow of a hydrocyclone. “This is not the case for dense medium cyclones, however. The operating pressure or head remain constant in dense medium separation, and the separation efficiency of the unit cannot be changed by adjusting the size of the vortex finder or the spigot,” he adds.

The supplier designs the DMC based on the ore body densities and the separation requirements, selecting a dense medium that delivers the low-density material to the overflow and the high densities to the underflow. “Unless there are significant changes to tonnages or the densiometric profile of the ore body, there should not be any need to change the DMC units themselves. Any adjustments should be made externally, to the dense medium and the feed parameters, for example,” Bekker suggests.

Dense medium cyclones and coal quality changes

“South Africa’s coal quality used to be very good. When using a dense medium cyclone in the early years, this resulted in easy separation, typically with 70% being coal at the overflow and only 30% being rejected as waste rock to the underflow. But we are now dealing with much lower grade coal ore, so the ratio is more or less the other way around, 70% being rejected as waste material through the spigot and only 30% being separated out as coal at the vortex finder in some cases,” Bekker notes.

“This causes capacity issues at the spigot in handling the larger volumes of waste materials and a decision has to be made as to whether to make the spigot bigger or to replace the dense medium cyclone with a bigger one,” he adds.

He says that certain design ratios apply between the cyclone diameter, the vortex finder, the spigot and the inlet diameter. If the cyclone diameter is D, for example, then the vortex finder is normally 0.43×D and the spigot can be anything between 50% and 70% of the vortex finder diameter. The standard inlet opening of a dense medium cyclone is normally 20% of the cyclone diameter.

“If the inlet opening is made bigger, more volume can be introduced into the unit, but this reduces the residence time inside the cyclone, which results in more misplacement of waste in the overflow and/or coal in the underflow, particularly of the case where the near density materials (NDM) is high. Near density material is defined as the amount of material present around the expected cut density in a band of +/- 0.1 RD units e.g. If the cut density is RD1.6, then the material present in the density range of RD1.5 to RD1.7 would be classified as near density material.

If the percentage of NDMs is very high, let’s say above 65%, then separation is difficult. Easy separation has anything between 20 to 25% NDMs and for medium density cyclones treating very good quality coal, NDM percentages can be as little as 2% in some of Multotec’s overseas operations.

“But here in South Africa, we use a lot of low-grade coal and it is quite difficult to distinguish clearly between the good coal and the waste. There are operations that can have up to 90% of the ore coming into the dense medium cyclone that is classified as near density material, making separation very difficult,” Bekker tells MechChem Africa, adding that cyclones for these applications need to be sized correctly, with very accurate feed conditions.

Diamonds and pre-concentration prior to milling

Alongside coal, Bekker says that dense medium cyclones are widely used as part of diamond pre-processing from run-of-mine ore prior to sorting. “Here only 1 to 2% of the inflow is diamond bearing and this passes through the spigot. The rest all goes out through the overflow. And if the underflow ratio goes up to just 4 or 5%, it becomes a problem because of the very accurate diamond sorting processes that must take place downstream of the cyclone, which can easily become overloaded,” says Bekker.

In a similar way, he adds that dense medium cyclones are now being looked at to pre-concentrate iron ore; manganese; and for some PGM and copper applications. “The idea is to remove waste rock before sending the product to the grinding mill, so that all the milling energy is focused only on the valuable target material, which is an interesting cost saving and productivity increasing concept,” he adds.

“While a small percentage of the valuable material is likely to be lost to the DMC, if you can recover, 90 to 95% of the valuables from 30% of the total ore mass, then the savings and productivity improvements from reduced milling can far outweigh this loss,” he points out.

“At Multotec we are process specialists who offer a variety of different minerals processing solutions and combinations. We spend time with the clients, building trust and sharing knowledge, regardless of any associated order or monetary value. And because we are an OEM supplier of several different technologies, we are able to steer our clients towards the right combination of technologies, whether those involve hydrocyclones, dense medium cyclones or combinations of several technologies.

“Every system we design and build is customised for specific client needs to be fit-for-purpose – and we take responsibility for ensuring this is the case,” Ernst Bekker concludes.

PumpPowerAUS/PEMO

Horizontal slurry pumps are indispensable in moving abrasive and corrosive liquids efficiently. These pumps are designed to handle liquids containing solid particles, making them the right choice in various industries such as mining, construction, and wastewater treatment. Here below you’ll find all the Pemo horizontal slurry pumps, while in the news section we go deeper into the definition, types, uses, and advantages of horizontal slurry pumps.

Pemo horizontal slurry pumps

Pemo’s horizontal slurry pumps are specifically designed for specific industry and purpose, we can build it in the V-Belt and Direct Transmission versions. All the Pemo horizontal pumps have the sealing system that consists of mechanical seals, with faces that are made of Tungsten Carbide (widia) or of Silicium Carbide. Lubrication of the mechanical seals, when there is a pair per pump, can be made with flushing water at a determined pressure, depending on the version, or with water/glicole by means of different closed circuits with natural or forced circulation. Instead, lubrication of the bearings is made with grease or oil.

Pemo Pumps models

Pemo Pumps has three different series of horizontal sludge pumps:

AO-AO/AD Series are standard horizontal pumps with frontal inlet. Based on our standards, the maximum available pressure should never exceed 2 bar (29 psi). Since there is only one
mechanical seals
these models are used to pump only water like fluids with almost no abrasive particles.

AO/TD – AO/TD/AD Series are horizontal pumps with frontal inlet and double mechanical seals, flushing must be done at a pressure that must be about 1 bar (15 psi) higher than the slurry outlet pressure. They can be used to pump abrasive and/or acid liquids. Maximum outlet pressure should not exceed 3-4 bar (45 – 60 PSI). Designed for heavy duty slurry and/or acid applications, these pumps have capacities from 1 to 1500 m3/h (5 to 6613 gpm).

AO/AB – AO/AB/AD Series are one of the most popular and distinctive products of the Pemo Pumps range. Thanks to the side inlet, the maximum pressure that the mechanical seals see is the fluid inlet pressure, greatly increasing life expectancy. For this reason, flushing must be done at a pressure that must be about 1 bar (15 psi) higher than the slurry inlet pressure instead. When pumping acid liquids, the shaft and the mechanical seals chamber can be made of special alloys.

Designed for slurries and/or acid applications, these Pemo pumps are truly unique! Maximum particle size is 2 mm though this is dependent on the specific application, capacities are from 1 to 900 m3/h (5 to 3,968 gpm), and maximum discharge head is 90 m (295 ft) in the Hardalloy PEMO design.

Primary markets

These are the primary markets where Pemo horizontal slurry pumps are used, we also can provide to our clients references and case studies.

Mining, Quarries, and Mineral Extraction
Aggregate Industry
Chemical Industry
Food Industry
Industrial Wastewater Treatment.

AO/TI and AO/TD Series, main characteristics

  • Designed for heavy duty slurry and/or acid applications.
  • These are end suction slurry pumps with single or double mechanical seals.
  • Capacities from 1 to 1500 m3/h (5 to 6613 gpm).
  • Usually maximum discharge pressure should not exceed 3 bar or 43 psi.

AO/AB Series, main characteristics

  • Designed for slurries and/or acid applications.
  • The heart of the PEMO product line, the AO/AB Series pumps are truly unique. Due to the side inlet, the maximum pressure the mechanical seal will see is the fluid inlet pressure, greatly increasing life of the seal.
  • When pumping acid liquids, the shaft and the mechanical seal housing can be made of special alloys.
  • Maximum particle size is 2 mm though this is dependent on the specific application.
  • Capacities from 1 to 900 m3/h (5 to 3,968 gpm).
  • Maximum discharge head is 90 m (295 ft) in the Hardalloy PEMO design.

Pemo Pumps is an Italian excellence in the custom pumps market. With a production 100% made in Italy, 50% of Pemo Pumps revenues comes from direct sales worldwide. Just one third of our sales are to Italian companies for direct use and for selling worldwide. Pemo Pumps has subsidiaries, representatives, and agents in 20 Countries and has more than 4,000 customers in the World.

Contact today our consultants to learn more about the complete range of Pemo Pumps.

Precisionscreen’s sand solutions are made for Australia

by Adam Daunt

Precisionscreen

Precisionscreen designs and manufactures its sand washing equipment in Brisbane. Image: Precisionscreen

Share on FacebookShare on Twitter

The sand-washing range from Precisionscreen is made for Australian conditions with options for all types of operators and contractors.

Demand for natural or manufactured sand is rising in the Australian market, so having the right equipment is essential.

Precisionscreen has developed its sand-washing equipment range over several years to ensure it could help the smallest of sand producers to the larger players in the sector.

Jonny McMurtry, chief operating officer at Precisionscreen, told Quarry he believed there would likely be continual strong demand for the material.

“There has been an increase in demand for sand washing equipment as I think there is increased demand for washed sand in the market,” he said.

“As the volume of infrastructure continues to be there and climb, the requirement for sand isn’t going to go away.”

The market for washed sand and manufactured sand is becoming more diverse as quarries explore how they can use the material to either expand their offering to the market or add new revenue streams.

Original equipment manufacturers like Brisbane-based Precisionscreen have developed a wide range of sand-washing equipment to suit specific applications and help customers take advantage of the growing demand. In one case, Precisionscreen worked with Victorian-based construction materials supplier site to create a sand-washing solution for their manufactured sand application. The company has employed the use of a sand screw from Precisionscreen to create a manufactured sand using washed crusher dust.

“Our sand washing equipment has been developed over a number of years and we offer different machines for different applications or customer price ranges or throughputs,” McMurtry said.

Precisionscreen has built out its range of sand washing equipment to provide solutions for customers from the first stage of washing to the final stage. The company manufactures all its sand washing equipment at its headquarters in Wacol, Brisbane which gives it the distinction of being Australian made.

The company’s adaptable wash kits have a range of customisable features to tailor the kit to the customer’s specific application. The Precisionscreen wash kit can range from single deck to two or three-deck kits which are built on the screen box.

Each deck has multiple spray bars with several spray nozzles to rinse the product being processed.

Operators can finely control the individual gate valves to each bar which provides enhanced control and excellent washing coverage.

“The wash kits as part of our screen boxes are probably the first step for sand washing,” McMurtry said.

“We sold quite a few of those this year, predominantly for sand washing but even washing pebbles or rinsing different products to remove dust has been in demand.”

Precisionscreen Sandscrew has also been in demand from customers across Australia due to its versatility. It can work alongside Precisionscreen’s wash kits or other wash plants to help dewater and classify sand products.

The sand screw has a hydraulic drive and features a mobile-wheeled axle as well as an adjustable overflow weir. The Sandscrew can be operated off the Precisionscreen’s screening plant powerpack.

The spiral screw helps separate heavier particles as they sink to the bottom of the trough after being dragged through the trough by the spiral screw. Dewatering occurs throughout the trough until the finished product is discharged via a chute.

“Our Sandscrews have been quite a hit just due to the adaptability. It can work with existing screening plants or existing applications if needs be. We’re one of the few manufacturers that makes our sand screws semi-mobile so it can couple up with existing systems if needed,” McMurtry said.

“The sand screw is probably on the lower end with throughput and cleanliness of sand but it has performed very well [in creating] a manufactured sand where it is quite suitable and economical for that type of application.”

Precisionscreen has a wide range of sand washing solutions for customers. Image: Precisionscreen

Precisionscreen has also created a modular sand washing plant which combines a galvanised 10×5 two-deck wash screen with a SRD180 bucket wheel dewaterer and a fines recovery pod to create a one-stop solution for sand producers.

It allows operators to create up to three different sand fractions and accept material from a dry screening process via conveyor belt or cyclone mounted above the screen. The SRD180 bucket wheel dewaterer collects sand particles from slurry materials in a wet screening process with its primary responsibility being to pick up heavier particles of sand as they sink to the bottom of the tank. It can manufacture coarse and fine grade sands simultaneously. It features a submerged back screw which helps float off unwanted silts while its large water overflow area and polyurethane bucket inserts provide a sizeable dewatering capacity.

The FRP has a 250mm cyclone on-board, discharging heavy particle sand onto the high-frequency dewatering screen for draining. The screen helps remove unwanted materials, excess water or organic materials from the sand material. The cyclone and screen are hydraulically driven and designed to work with Precisionscreen’s washing plants.

McMurtry said the SRD and FRP had benefits even as standalone products for Australian operators.

“The SRD180 or the FRP gives a greater throughput and a cleanliness of the sand as well and that’s where it comes into its own.

“If you have a high silt content and you need to float off a lot of that bottom end product in that super fine sand, that’s when the likes of the SRD or FRP comes into its own,” he said.

“If a customer has water restrictions or low access to water that is where the FRP can allow any residual water to be taken off your sand product quite quickly and easily. Or it can use the cyclone to take out the super fine sand to recycle that water quickly.” •

For more information, visit precisionscreen.com.au

PumpDim™ software

The PumpDim™ software streamlines the complexities of accurately modeling how a slurry pump will perform in a system. The software takes into account particle size distribution, percent solids of the slurry, liquid viscosity, and the piping conditions around the slurry pump to accurately size the ideal pump for the given conditions.

✅ Are you working on a brand new plant or upgrade? PumpDim™ can be used to determine the best slurry pump.
✅ Have an existing plant with slurry pumps? PumpDim™ can model how the slurry pumps are performing.
✅ Curious to see the hydraulic performance curves of Metso’s slurry pumps? This can be found in PumpDim™ with the Performance curve viewer.

https://www.metso.com/campaigns/pumpdim-slurry-pump-selection/?utm_source=facebook&utm_medium=social&utm_campaign=2024-min-social-media&utm_content=slurry-pump-selection

A winner for Weir

A Warman MCR 760 installed at a copper mine in Chile. Image: Weir

Weir will supply its Warman slurry pumps and Cavex hydrocyclones to Teck’s Highland Valley copper (HVC) mine in Canada in a new contract award.

Teck is completing its HVC mine life extension (MLE) project, aiming to extend the mine’s operational life through enhancing site infrastructure. The project is expected to yield around 1.95 million tonnes of additional copper over its lifespan.

The Warman MCR 760 pump is a cornerstone of the project, holding the title of the largest mill circuit pump in North America.

Designed to maximise wear life in arduous mill duties and facilitate easy and safe maintenance, the Warman MCR 760 pump addresses the global trend of declining ore grades that require increased throughput for economical mineral recovery.

Weir will also supply its Cavex 800CVX and 650CVX hydrocyclones for the MLE project. The solution was chosen thanks to its consistently high classification efficiency, capacity and low maintenance requirements.

A Warman MCR 760 slurry pump.
Image: Weir

“Weir has a proven track record of supplying and supporting the largest, highest capacity mill pumps on the market,” Weir divisional senior product manager, pumps Quinton Sutherland said.

“Designing, manufacturing, and supporting pumps of this scale presents unique technical and engineering challenges, which is why Weir’s team of experts, drawing on decades of experience supporting customers across the globe, are the best choice when deciding who to trust with the most critical mill circuit operations.”

Weir director, capital sales North America Phil Blondin said the company priorities being close to its customers, wherever they are in the world.

“We have a service centre in Kamloops – a close drive to HVC – and a local team that can provide service and maintenance support, as well as an inventory program that encompasses the lifecycle of the products we supply,” Blondin said.

“This is the first mill pump this large in North America and, while Weir has manufactured and installed pumps this size in other parts of the world, we recognise that having a service network to support customers at every stage of the project is an essential part of what we’re offering.”

Subscribe to Australian Mining and receive the latest news on product announcements, industry developments, commodities and more.

Weir locks in deal with 100-year mine

Kelsie Tibben

The Weir WARMAN slurry pump. Image: Weir

The Weir Group, a global mining technology leader, has been awarded a £25m ($48.2 million) contract to provide sustainable solutions to the next phase of OCP Group’s Benguerir and Louta greenfield phosphate projects in Morocco.

The order, which includes the company’s WARMAN slurry pump and CAVEX hydrocyclone technology, will support the continued construction of the Louta project and the trebling of production from the Benguerir project.

Weir has previously provided similar separation and de-sliming solutions also based on its WARMAN and CAVEX technology.

The Benguerir expansion will start up following the initial phase of the project which has scheduled first production in 2024, with an estimated total mine life of more than 100 years.

“We are pleased to have secured this major contract. It represents a strong endorsement of our WARMAN and CAVEX ranges that provide energy efficient separation at scale to support our customer’s productivity and sustainability goals,” Weir chief executive officer Jon Stanton said.

“Along with our industry-leading solutions, we promise our customers world class service; our local team are delighted to continue to deliver for OCP as they commission the initial phase at Benguerir and look to expand these exciting projects.”

After commissioning of the equipment, aftermarket support will be provided via Weir technical experts from the company’s Moroccan service centre, which is located close to the projects.

Founded in 1871, The Weir Group is one of the world’s leading engineering businesses with a purpose to make its mining and infrastructure customers’ operations more sustainable and efficient.

Weir’s highly engineered technology aims to enable critical resources to be produced using less energy, water and waste while reducing customers’ total cost of ownership.

Subscribe to Australian Mining and receive the latest news on product announcements, industry developments, commodities and more.