In crushing and screening, Astec is always evolving

by William Arnott

Astec

Astec has designed 20 new mobile tracked crushing and screening plants. Image: Astec

Share on FacebookShare on Twitter

Quarry speaks with Astec Industries’ Adam Gordon to find out how innovative technologies have unlocked a brand-new design of crushing and screening equipment.

Astec Industries does not want to stand still. If it does not stay up to date with the latest innovations and improvements, it risks being surpassed in the competitive original equipment manufacturer (OEM) market.

“If you don’t incorporate improvements into your machinery, someone else will,” Astec Industries business line manager Adam Gordon told Quarry. “That means we have to stay innovative.”

This drive to evolve is what inspired the company to design 20 new mobile tracked crushing and screening plants.

Based on tried-and-tested machinery that has proven popular in the US, the new range of plants has been designed to be easier to maintain.

The new range has also incorporated improvements in engines, hydraulics, and materials.

Gordon said that in an industry where heavier usually means longevity, the new range has reduced weight to make it easier to move.

“It’s not just our industry that has seen rapid development, it’s the whole world. There are all new specialty steels with unique performance characteristics that allow us to design these machines even better,” he said.

“Some of the heavy-weight sections can be reduced in thickness because the steel has gotten much stronger.

“With greater strength characteristics, you can reduce the weight of the steel section, which means more flexibility and less impact on the ground.

“Similarly, if you can make your conveyors more efficient and require less power, then your drives can be smaller. Your hydraulic flow can be reduced thanks to more efficient pumps.

“All of these small improvements add up to about a 10 to 15 per cent improvement in productivity and yield.”

Mobile equipment offers significant benefits for Australia’s quarrying sector. Image: Astec

Finding new ways to improve efficiency for customers is key for Astec. At the end of the day, the company’s clients are looking to reduce their cost per tonne, which means using the most cost-effective equipment possible.

Mobile equipment also offers significant benefits for Australia’s quarrying sector.

Gordon said they offer an effective way of avoiding lengthy approvals.

“It can be difficult to get approvals in this industry for fixed infrastructure,” he said. “Setting up a fixed plant is also a big capital investment, and securing a lender can be a headache.

“Mobile equipment is fast to set up on a site, meaning that equipment can get to work as soon as possible.”

This flexibility is especially important for smaller quarry operations. Often, the profit margins are much tighter, so finding the right size of equipment is key to getting the economics right.

Mobile gear can also be moved to different sites, creating the potential for smaller production volumes to become more economical.

Astec
Astec has a global network of facilities to provide customers with support. Image: Astec

Australian support

The first few of the new machines, the SF-20 Tracked Screeners, have already been rolled out. Three have already been in the field for thousands of hours to ensure they can handle all the challenges operating in a quarry can throw at them.

This robust field testing helps Astec find the unexpected and is important to improving the designs.

Astec has service facilities in Brisbane and Melbourne, with technicians located throughout the country to support its asphalt plants and crushing equipment products. Most of these service technicians are cross-trained, enabling them to handle any issue that may arise across Astec’s broad range of products.

Gordon said it’s important to provide high-quality, fast-response service in the quarry sector.

“When a piece of equipment breaks down, it’s not just affecting one thing – it impacts the entire process,” he said.

“The loaders, the excavators, the tracked equipment – all of it comes to a halt waiting for the problem to be solved. If you’re working with something like an asphalt mixer, there’s also a time limit before the material begins to thicken and solidify. That’s why reliability is so important for our customers. If there’s a breakdown, they’re losing out on productivity. The better we can support our customers, the more likely they will support us in return.”

Repeat business is an important part of Astec’s goal of growing six times larger by 2030.

The company recently acquired TerraSource, a specialist manufacturer of complementary equipment, providing new opportunities for the company.

This international growth has given Astec the support it needs to start rapidly expanding across Australia.

Gordon said the tracked equipment market was competitive, which is why having an efficient production process were vital.

“Each company is trying to continually evolve, offering greater features and benefits while improving their production volumes while reducing their manufacturing costs,” he said.

To reach this, Astec has fast-tracked the growth of its manufacturing facility in Omagh, Northern Ireland.

The country has long been a hub for crushing equipment manufacturing, and by expanding its presence there, Astec has freed up its US factories, which had previously supplied the global market.

Gordon said having its manufacturing facilities in Northern Ireland was the best for ease of manufacturing and logistics.

“If you look at Northern Ireland, around 7000 tracked crushers and screeners are manufactured and shipped from there to the world market,” he said. “That means there is a lot of expertise we can harness, as well as the auxiliary equipment that is needed for tracked equipment. At the moment, we have 19 pieces of tracked equipment in our Australian inventory, and this is growing all the time. We’re excited to start showing off what it can do.” •

For more information, visit astecindustries.com

How XCMG’s mobile crushers elevate operational efficiency徐工移动式破碎机如何提高运营效率

Staff writer  特约撰稿人

XCMG’s mobile crushers are compact, enabling easy transportation from site to site. Image: XCMG
徐工的移动式破碎机结构紧凑,便于从一个地点到另一个地点的运输。图片:徐工

XCMG’s new mobile crusher range is underpinning faster, more efficient mining operations.
徐工的新型移动式破碎机系列正在为更快、更高效的采矿作业奠定基础。

When you think of mobility in the mining and construction industries, chances are your mind jumps to transport solutions, machinery relocation, or agile operations planning.
当您想到采矿和建筑行业的移动性时,您的思绪很可能会跳到运输解决方案、机械搬迁或敏捷运营规划上。

But what about crushing?   但是压碎呢?

In a sector where power and performance often come in bulky and stationary packages, XCMG is shifting the paradigm.
在动力和性能通常采用笨重且固定封装的领域, 徐工正在改变范式。

With the release of its powerful line-up of mobile crushers – XPE0810, XPE0912, XPF1214, and XPY1100 – XCMG is making it clear: might and mobility can go hand in hand.
随着其强大的移动式破碎机系列(XPE0810、XPE0912、XPF1214 和 XPY1100)的发布,徐工集团明确表示:力量和机动性可以齐头并进。

From quarries to remote mining operations, infrastructure projects to demolition sites, these crushers are built for action.
从采石场到偏远采矿作业,从基础设施项目到拆除现场,这些破碎机都是为行动而生的。

They’re fast, flexible, fuel-efficient, and formidable. But beyond the specs and steel, the crushers represent something bigger: a move towards smarter, leaner, more responsive crushing systems that adapt to the demands of modern mine sites.
它们快速、灵活、省油且强大。但除了规格和钢材之外,破碎机还代表着更大的东西:向更智能、更精简、反应更灵敏的破碎系统迈进,以适应现代矿场的需求。

Let’s break it down.  让我们来分解一下。

Mobility meets muscle  机动性与肌肉的结合

Traditional crushers demand infrastructure, pads, foundations, power sources, and logistical planning.
传统破碎机需要基础设施、垫片、基础、电源和物流规划。

The introduction of XCMG’s mobile crushers mean those limitations are a thing of the past. Mounted on robust tracks and engineered for seamless transportation, these machines are redefining what it means to be site ready.
徐工移动式破碎机的推出意味着这些限制已成为过去。这些机器安装在坚固的轨道上,专为无缝运输而设计,正在重新定义现场就绪的含义。

Whether it’s the compact and agile XPE0810, the mid-range XPE0912 workhorse, or the heavy-hitting XPF1214 and high-efficiency XPY1100, this range provides a crushing solution for every scenario.
无论是紧凑敏捷的 XPE0810、中档 XPE0912 主力,还是重磅 XPF1214 和高效 XPY1100,该系列都为各种场景提供了粉碎解决方案。

What unites them all? Their precision design, field-tested durability and a relentless pursuit of efficiency that has become a hallmark of the XCMG brand.
是什么将它们结合在一起?他们的精密设计、经过现场测试的耐用性和对效率的不懈追求已成为徐工品牌的标志。

Balancing power and precision
平衡功率和精度

When you need performance without sacrificing mobility, the XPE0810 delivers. Built for demanding workloads, this mid-size jaw crusher offers the ideal balance between power, portability, and efficiency.
当您需要性能而不牺牲移动性时,XPE0810 可以满足您的需求。这款中型颚式破碎机专为要求苛刻的工作负载而设计,在动力、便携性和效率之间实现了理想的平衡。

Engineered for tough conditions, the XPE0810 thrives on job sites where reliability and productivity are non-negotiables. From reinforced concrete to hard rock, it handles a wide range of materials with ease, making it a go-to solution for contractors who need results.
该 XPE0810 专为恶劣条件而设计,在可靠性和生产力不容谈判的工作现场蓬勃发展。从钢筋混凝土到硬岩,它可以轻松处理各种材料,使其成为需要结果的承包商的首选解决方案。

Key features include:  主要功能包括:

  • being compact enough for easy transportation and powerful enough for large jobs
    足够紧凑,便于运输,功能强大,适合大型作业
  • rapid set-up and intuitive operation
    快速设置和直观作
  • robust jaw crushing performance
    强大的颚式破碎性能
  • suited to construction sites, recycling yards, quarry and mining operations.
    适用于建筑工地、回收场、采石场和采矿作业。

The versatile workhorse  多功能主力

Step up a level to the XPE0912, a mobile jaw crusher engineered for higher output and more demanding tasks.
更上一层楼,XPE0912,这是一款移动式颚式破碎机,专为更高的产量和更苛刻的任务而设计。

With a larger feed opening and increased throughput, the XPE0912 is perfect for contractors and mining operators who need a robust, multi-purpose crusher that can adapt on the fly.
该 XPE0912 具有更大的进料口和更高的吞吐量,非常适合需要坚固耐用且可动态适应的多用途破碎机的承包商和采矿运营商。

The XPE0912 mobile jaw crusher. Image: XCMG
XPE0912 移动式颚式破碎机。图片:徐工

Whether operators are breaking down blasted rock or reprocessing concrete debris, the XPE0912 keeps sites moving.
无论操作员是分解爆破的岩石还是再处理混凝土碎片,XPE0912 都能让现场保持运转。

Key features include:  主要功能包括:

  • a heavy-duty jaw plate design
    重型钳口板设计
  • hydraulic adjustment for quick changeovers
    液压调节,可快速转换
  • remote control mobility  远程控制移动性
  • suited to medium to large crushing volumes.
    适用于中到大破碎量。

This is a machine that can easily shift from job to job without skipping a beat. The XPE0912 is rugged enough for tough conditions, and smart enough for dynamic workflows.
这是一台可以轻松地从一个工作转移到另一个工作而不会错过任何一个节拍的机器。该 XPE0912 足够坚固,可以应对恶劣的条件,并且足够智能,可以应对动态工作流程。

The heavy-hitter  重量级人物

The XPF1214 mobile impact crusher is built for productivity. With a powerful rotor and large crushing chamber, it delivers aggressive performance for high-volume operations.
XPF1214 移动式反击式破碎机专为提高生产率而设计。凭借强大的转子和大型破碎室,它为大批量作业提供了积极的性能。

It’s ideally suited for limestone, concrete, asphalt, and other medium-hard materials, delivering uniform product size with exceptional shape.
它非常适合石灰石、混凝土、沥青和其他中等硬度材料,提供均匀的产品尺寸和卓越的形状。

But the XPF1214 isn’t just about brute force. It’s loaded with intelligent features that reduce downtime and boost productivity.
但 XPF1214 不仅仅是蛮力。它加载了智能功能,可减少停机时间并提高生产力。

Adjustable aprons, fast maintenance access, and dust suppression options all contribute to a machine designed for real-world performance.
可调节围裙、快速维护访问和粉尘抑制选项都有助于打造专为实际性能而设计的机器。

Key features include:  主要功能包括:

  • high-capacity impact crushing
    大容量冲击式破碎
  • an advanced hydraulic opening mechanism
    先进的液压开启机构
  • flexible feed size and output adjustments
    灵活的进料尺寸和产量调整
  • suited to quarry, roadwork, and recycling applications.
    适用于采石场、道路施工和回收应用。

Cone crusher for consistency and control
圆锥破碎机,确保一致性和控制

Rounding out the range is the XPY1100, a mobile cone crusher engineered for precision and consistency.
该系列的最后一款产品是 XPY1100,这是一款专为精度和一致性而设计的移动式圆锥破碎机。

Cone crushers have always been valued for their ability to produce high-quality aggregates, and the XPY1100 is no exception.
圆锥破碎机一直因其生产高质量骨料的能力而受到重视,XPY1100 也不例外。

With intelligent control systems, robust wear parts, and premium gradation capabilities, this model is ideal for secondary and tertiary crushing stages in mining and aggregate production.
该型号具有智能控制系统、坚固的易损件和优质的级配能力,是采矿和骨料生产中二级和三级破碎阶段的理想选择。

Key features include:  主要功能包括:

  • hydraulic cone technology with overload protection
    带过载保护的液压锥体技术
  • automatic clearance adjustment
    自动间隙调整
  • high reduction ratio and cubical product shape
    高减速比和立方体产品形状
  • smooth integration with other XCMG crushers for multi-stage setups.
    与其他徐工破碎机顺利集成,实现多级设置。

Operators choose the XPY1100 for its stability and control, while managers appreciate its uptime, output, and low operating costs.
运营商选择该 XPY1100 是因为它的稳定性和控制性,而管理人员则欣赏其正常运行时间、产量和低运营成本。

It’s a high-performance machine that brings balance and finesse to the crushing process.
它是一款高性能机器,可为破碎过程带来平衡和技巧。

Why choose XCMG mobile crushers?
为什么选择徐工移动式破碎机?

There are plenty of crushing options on the market, but here’s why XCMG’s lineup stands out.
市场上有很多粉碎选择,但这就是徐工产品线脱颖而出的原因。

True mobility: All four crushers are mounted on high-strength tracks and feature powerful travel motors, making them easy to relocate across job sites, even in rugged terrain. No waiting for transport and no wasted hours.
真正的机动性: 所有四台破碎机都安装在高强度轨道上,并配备强大的行走电机,即使在崎岖的地形中,也可以轻松地跨作业现场重新定位。无需等待运输,也无需浪费时间。

Plug-and-play simplicity: Set up is quick and intuitive, reducing downtime between deployments. Within hours, your team can be up and running, with minimal training required.
即插即用的简单性: 设置快速直观,减少部署之间的停机时间。在几个小时内,您的团队就可以启动并运行,只需最少的培训。

Reliability where it counts: XCMG’s engineering legacy means these machines are built to last. Reinforced frames, high-quality wear parts, and intelligent hydraulic systems ensure dependable performance, even under punishing workloads.
可靠性 :徐工的工程传统意味着这些机器经久耐用。加固的框架、高质量的易损件和智能液压系统确保了可靠的性能,即使在严酷的工作量下也是如此。

Low operating costs: Efficient power systems, fuel economy, and low maintenance requirements translate to better margins and lower cost-per-tonne. These crushers are designed to crush your materials, not your bottom line.
低运营成本: 高效的动力系统、燃油经济性和低维护要求转化为更好的利润和更低的每吨成本。这些破碎机旨在破碎您的材料,而不是您的底线。

Smart integration: All models can be easily integrated into multi-stage crushing circuits or paired with XCMG’s screening and conveying equipment for complete material processing solutions.
智能集成: 所有型号都可以轻松集成到多级破碎回路中,或与徐工的筛分和输送设备配对,以获得完整的物料加工解决方案。

Today’s mine sites are fast-paced and ever-evolving, so operators need machines that can keep up.
当今的矿场节奏快、不断发展,因此操作员需要能够跟上的机器。

XCMG’s mobile crushers are loaded with features that make life easier for crews on the ground, including remote diagnostics for quick troubleshooting, user-friendly control interfaces with touchscreen displays, safety-first design with accessible maintenance points and emergency stop systems, and eco-mode options for fuel-conscious operators.
徐工的移动式破碎机具有让地面工作人员更轻松的功能,包括用于快速故障排除的远程诊断、带有触摸屏显示器的用户友好控制界面、带有无障碍维护点和紧急停止系统的安全第一设计,以及为注重燃料的操作员提供生态模式选项。

Every detail is designed to maximise uptime, optimise throughput, and minimise complexity.
每个细节都旨在最大限度地延长正常运行时间、优化吞吐量并最大限度地降低复杂性。

Real results in the field
现场的实际结果

It’s one thing to talk specs, it’s another to deliver results in high-pressure environments.
谈论规格是一回事,在高压环境中交付结果是另一回事。

Operators are reporting significant time savings thanks to fast setup and simplified mobility between crushing zones.
运营商报告说,由于快速设置和简化了破碎区之间的移动,可以节省大量时间。

In multi-stage applications, the pairing of jaw and impact crushers has proven especially effective in cutting down material handling steps and streamlining workflow.
在多级应用中,颚式破碎机和反击式破碎机的配对已被证明在减少物料搬运步骤和简化工作流程方面特别有效。

Teams have also noted reduced wear rates and smoother output gradation when switching to XCMG’s mobile systems, particularly in sites with variable feed material. The result? Better efficiency, fewer delays, and a noticeable boost in overall production performance.
团队还注意到,在切换到徐工的移动系统时,磨损率降低,输出级配更平滑,特别是在进料可变的现场。结果?效率更高,延迟更少,整体生产性能显着提高。

As global construction and mining trends evolve, so do the demands on equipment. Flexibility, efficiency, and sustainability are no longer optional – they’re expected.
随着全球建筑和采矿趋势的发展,对设备的需求也在不断变化。灵活性、效率和可持续性不再是可选的,而是人们所期望的。

With its mobile crushing range, XCMG is not just meeting these expectations – it’s setting new ones. These machines provide the performance, intelligence, and adaptability that modern mining operations require.
凭借其移动破碎范围,徐工不仅满足了这些期望,还树立了新的期望。这些机器提供现代采矿作业所需的性能、智能和适应性。

In short? XCMG is crushing it in every sense of the word. 
总之?徐工集团在各个方面都碾压了它。

This article appeared in the October issue of Australian Mining magazine.
本文发表在 《澳大利亚矿业》杂志 10 月号上。

Onetrak builds on trusted partnerships to support quarries

by William Arnott

Onetrak

Onetrak is the Australian distributor of Anaconda Equipment. Image: Onetrak

Share on FacebookShare on Twitter

Family businesses from around the globe are working together to deliver crushing equipment tailored to support Australian quarries.

Paul Kerr has spent more than 30 years in the quarry equipment business. During this time, he has visited dozens of factories, learning what makes them tick and how they build equipment for the Australian environment.

He brings this experience to his role as Onetrak’s national manager for crushing and screening. His responsibility is to liaise with original equipment manufacturers (OEMs) for the Australian-based family business.

One of these OEMs is Anaconda, which itself is a family business based in Northern Ireland. It specialises in designing, manufacturing, and supplying trommels, crushers, and screens for the material handling sectors.

Originally founded in 2005 as sub-contractor specialists, Anaconda was acquired by another family business – the McLanahan Corporation.

“It’s dynamic to work with three different family businesses, across three different continents,” Kerr told Quarry.

“We can get technical support from the factory – and not just from Northern Ireland. Reciprocal engineers in the United States means we have someone available across 16 hours a day.

“While they support us, we can also support them.”

Anaconda is a family business based in Northern Ireland. Image: Onetrak

The Australian quarry industry has unique demands. This is why Kerr was an ideal person to work alongside Anaconda’s design team. He said the three main issues facing Australian equipment are the heat, the dry climate, and geographical remoteness.

“We’re quite unique as a market segment, and we’re an area where Anaconda wants to make a difference,” Kerr said.

“Heat mostly affects screens. They’re hydrostatic and hydraulically driven. High temperatures can affect the longevity of seals and hoses, which can cause a loss of efficiency.

“There’s also a need to make sure the viscosity of the oil is the right level, and heat plays a major role. It’s important to make sure that every component is appropriate for the hot weather and high ultraviolet radiation.”

A dry climate means dust ingress can become a major problem. If dust manages to get into bearings and seals, it can significantly reduce the reliability of a machine. Placement of the bearings can also reduce the risks of dust ingress. To address these issues, Kerr visited the Anaconda factory and spent three days working with the company’s engineers. During this time, he reviewed the Anaconda machinery bit by bit, consulting with the Northern Ireland team to make sure the products would be fit for Australian conditions.

Kerr had visited the company’s factory a decade ago and said the McLanahan Corporation’s investment had enhanced it.

“I’ve been to all of the major manufacturing facilities for this type of equipment in Northern Ireland, and Anaconda’s paint facility is the best I have seen,” he said.

“The software they use is on the cutting edge. With McLanahan’s help, they have been able to incorporate the latest technology, from hydraulic flow to finite element analysis.

“It is all used to make sure each machine meets the company’s standards, using the right materials.”

Onetrak is more than just the official Australian dealer for Anaconda. It is also part of the company’s consulting team for developing new products.

Kerr was impressed at how quickly his feedback was taken on board. Where it might have taken months for these changes to be made in another manufacturer’s process, Anaconda was able to update the design almost immediately.

“One of the most important things about Anaconda is its versatility. They’ve been around for a decade and have been improving their designs from day one,” Kerr said.

“They’ve designed machines that offer good value for money. The whole design concept is to create a dependable workhorse and have been able to make them even more reliable for the Australian market.”

This reliability is vital for Australian quarries. Not only is Northern Ireland on the other side of the world, but often quarries cannot afford to wait for replacement parts if a machine breaks down.

Anaconda was acquired by the McLanahan Corporation. Image: Onetrak

To solve this problem, Onetrak has eight branches that are spread across the country. Each branch carries important components and wear parts for the crushing and screening sector. In addition, a full fleet of trucks lets the company’s teams support quarries around Australia.

Its distribution centre in Melbourne supports these branches, and its partnerships in Asia, North America, and Europe help keep the stock of spare parts high.

Kerr said if anything needs to be done quickly, each branch has teams of specialists that can move quickly for emergency breakdowns.

“We’re continuing to expand,” he said. “We’re looking at opening up another office this year.”

“We’re also excited to celebrate a major milestone. This year, we will have delivered more than 500 Anaconda machines into Australia over the past decade.”

FLS’ future solutions empowering mines

Olivia Thomson

Advanced grinding technologies have the potential to significantly reduce energy consumption. Image: FLS

FLS is taking a holistic view of the entire metallurgical process to unlock value across recovery, efficiency and sustainability.

According to the International Energy Agency (IEA), mineral demand is expected to triple by 2050, fuelled by economic growth, urbanisation, and a rising global population.

At the same time, the green transition will further drive demand for minerals like copper and lithium.

While recycling will play a role here, FLS head of innovation and MissionZero Lucy England said mining will be the key driver.

“The mining sector will need to meet most of the increased demand for minerals, but it must do so while reducing its own environmental and social sustainability,” she told Australian Mining.

“Driven by this challenge, we at FLS are committed to delivering solutions that shape tomorrow’s mine.”

FLS is doing this via its MissionZero Mine, which aims to empower miners to maximise productivity while reducing environmental impact across the mineral processing flowsheet. 

At the heart of this approach is the company’s life-of-mine methodology, combining ore characteristics and customer needs to create flowsheets tailored to the mining site and application.

“At FLS, we like to say the secret is in the rocks,” England said. “By taking a holistic view of the entire metallurgical process and working in a fully integrated manner, we unlock value across recovery, efficiency, and sustainability.”

This approach enables operations to access lower-grade resources once deemed uneconomical, while reducing energy, water and land impacts.

“And it’s not just about having the best equipment – it’s about deploying it where and how it truly matters,” England said. “That’s how we help shape a mining industry that is more future-ready, responsible, and resilient.”

The FLS Minerals Testing and Research Centre is central to this approach. Located in Salt Lake City, Utah, the centre delivers state-of-the-art mineralogical and metallurgical testing services that underpin proper equipment selection, flowsheet design, plant troubleshooting, and research.

“No two deposits are the same, so this detailed testing ensures our flowsheets listen to the rocks to deliver an optimised, sustainable solution,” England said.

While FLS is most known for its equipment offering, its MissionZero Mine incorporates various innovations – some evolutionary, some revolutionary – that create a more sustainable mineral processing flowsheet of the future.

Several FLS REFLUX-based
solutions are now available to the wider mining sector. Image: FLS

This includes a suite of grinding technologies.

“Advanced grinding technologies, such as high-pressure grinding rolls (HPGR), vertical roller mills (VRM), the FLS Tower Mill (FTM), or our Eccentric Roll Crusher (ERC), have the potential to reduce energy consumption in certain mineral processing flowsheets compared to traditional grinding methods,” England said.

“They may have a particular role as ores get harder and more disseminated, requiring more control over particle size to ensure effective liberation.”

Meanwhile, dry grinding processes like HPGR and VRM also improve water management.

“Dry grinding means the water added during post-grinding repulping can be tailored to optimise recovery in the flotation circuit,” England said.

“This compares to traditional flowsheets, where the grinding circuit determines the water content of slurries.”

A revolution in separation

Beyond the grinding equipment, FLS’ REFLUX family of technologies offers the opportunity to revolutionise mineral separation efficiency while significantly reducing energy and other inputs.

“The REFLUX concept was developed in collaboration with the ARC Centre of Excellence for Enabling Eco-Efficient Beneficiation of Minerals at the University of Newcastle, New South Wales,” England said.

“Combining inclined lamella plates with a fluidised bed, the REFLUX concept improves recovery of off-size particles, offers high throughput in a much reduced footprint, and cuts energy and water consumption, perfectly aligning with our goal to do more with less.”

Several REFLUX-based solutions are now available to the wider mining sector, including the recently commercialised REFLUX Flotation Cell (RFC) and coarseAIR coarse particle flotation technology.

The latter is a lynchpin of the MissionZero Mine, as coarse particle flotation significantly reduces comminution energy consumption and facilitates faster and more effective dewatering, enabling filtered or dry tailings.

Other dewatering solutions under development include advances in the design of high-rate and paste thickeners with the introduction of:

  • new rake designs for thickened tailings
  • the AFP2525 tailings filter press, which uses high pressures and low cycle times to achieve significantly larger single-machine capacities
  • EcoTails filtered tailings
  • EcoPaste tailings.

“We are also investing in research to address the issue of chemical build-up in recycled process water, which can impact flotation efficiency,” England said, noting the company offers MaxR systems and reactor clarifiers to treat acid water and heavy metals build-up in tailings water streams.

FLS KREBS pumps are common sights at many mine sites. Image: FLS

Tailings are also increasingly being recognised as an essential source of mineral production, as mining companies reevaluate what is economically viable to extract.

“We expect to see greater reprocessing of tailings and a sharper focus on co-products in mineral processing flowsheets of the future using our REFLUX classifier (RC) and Reflux GradePro classifier,” England said.

Pumping sustainably

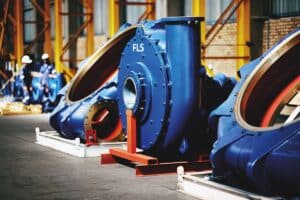
FLS KREBS pumps are common sights at many mines, but they might not be the first things called to mind when thinking about sustainability.

The significant energy consumption of KREBS pumps makes them an important target for improving energy efficiency and reducing energy-based carbon emissions.

“A recent life cycle assessment demonstrated that the adoption of KREBS pumps can lead to significant reductions in greenhouse gas emissions, primarily through their enhanced energy efficiency when in operation,” England said.

Driving this benefit is the pumps’ patented wear ring technology. According to FLS, this minimises recirculation, reduces grinding losses, and extends the lifespan of wear components.

“Performance studies conducted at real-world mining operations have documented energy efficiency improvements ranging from 5.3 per cent to 34.1 per cent, depending on operating conditions,” England said.

Hot on pyrometallurgy

An essential – if sometimes overlooked – part of the mineral processing flowsheet is pyrometallurgy.

FLS has a long and distinguished history in pyroprocessing, having pioneered the coal-fired rotary kiln in the late nineteenth century.

Today, the company’s Pyro Technology Centre of Excellence in Allentown, Pennsylvania is leading the development of more sustainable pyrometallurgical processes for producing critical minerals, particularly lithium.

“Our innovative lithium pyro island for spodumene concentrate conversion is the culmination of our most advanced technologies working together and features our state-of-the-art preheaters and coolers,” England said.

“It enables us to extract the maximum amount of lithium from the spodumene concentrate while minimising energy use and reducing carbon intensity – again doing more with less.

“Meanwhile, our multiple hearth furnace supports circularity in lithium processing (as well as cutting Scope 3 carbon emissions) by enabling lithium producers to recycle the lime used in lithium hydroxide production.

“Our pyrometallurgical equipment can also run using alternative (non-fossil) biofuels, hydrogen, and electric heating technologies.” 

Shaping the future, today

FLS firmly believes the future of mining is cleaner, more nature-positive, and more efficient.

“How individual mines achieve this will vary greatly,” England said. “There will be many flowsheets of the future, each contributing to a sustainable mining industry that not only provides the world with the minerals it needs to thrive.” 

This feature appeared in the June 2025 issue of Australian Mining.

Weir responds to the ‘big sand shortage’

by Guy Woodford

Weir at AGG-1 World of Asphalt 2025. Pictured left to right are Jarin Wildeman, Regional Sales Leader, North America; Magnus Skorvald, Global Product Manager – Crushers; Peter Brewitt, Global Product Manager Sand & Washing Plants; and Richard Uhlry, Area Sales Manager. Image/Guy Woodford

Weir at AGG-1 World of Asphalt 2025. Pictured left to right are Jarin Wildeman, Regional Sales Leader, North America; Magnus Skorvald, Global Product Manager – Crushers; Peter Brewitt, Global Product Manager Sand & Washing Plants; and Richard Uhlry, Area Sales Manager. Image/Guy Woodford

Share on FacebookShare on Twitter

Sand production is in the spotlight, and Weir is seizing the opportunity to solve producers’ sand supply challenges. Aggregates Business reports

Sand demand far outpaces supply, and construction material producers grapple with what industry experts acknowledge as the ‘big sand shortage’.

Sand is regarded as the second-most used resource after water, and its usage in a wide range of products from concrete to glass means demand seems to be ever-increasing.

Researchers at the University of Leiden in the Netherlands examined demand and found that growth in demand, especially in lower-income regions like Western and Eastern Africa and parts of Southern Asia, could rise by 269 to 500 per cent by 2060.

Their report stated: “International cooperation in sand extraction, material recycling and building technologies is essential in addressing the inequalities in access to shelter and resources for infrastructure. Better governance and planning will be needed to ensure future generations will have enough sand resources.”

The United Nations Environment Programme (UNEP) found in 2022 that sand extraction is rising at around six per cent annually, with around 50 billion tonnes extracted globally. The UNEP researchers concluded that this rate was “unsustainable.”

“Our sand resources are not infinite, and we need to use them wisely. If we can get a grip on how to manage the most extracted solid material in the world, we can avert a crisis and move toward a circular economy,” GRID-Geneva director at UNEP Pascal Peduzzi said at the time of the report.

“To achieve sustainable development, we need to drastically change the way we produce, build and consume products, infrastructures and services.”

These statistics have led to a conversation around sand production globally, how it is extracted, and potential alternatives. While this focus is not new, it has started to impact what technology companies are turning to in key markets for their sand production businesses.

Weir’s global product manager for sand and washing plants, Peter Brewitt, said the business had seen shifts in key markets, including the US and Europe, with its Sandmaster equipment.

“The Sandmaster type technology has been standard across Europe for the past 20 years, and the US has only started adopting it relatively recently,” he told Aggregates Business at AGG-1/World of Asphalt 2025 in St Louis, Missouri (25-27 March 2025).

A Weir Sandmaster wash plant. Image/Weir

“There has been a slight shift in the acceptance of the technology. There has been a concentration on the sandscrews and bucket wheels and things like that, but people are beginning to realise how much more efficient the hydrocyclone-based technology is, and we believe we have the best cyclones and pumps on the market.

“It cuts the sand better, is cleaner, and recovers more. Old sandscrew technology means you’re losing 10-15 per cent of the sand, but hydrocyclone technology is recovering most of that.”   

Weir released the Sandmaster in 2022 in response to customer feedback, which the original equipment manufacturer (OEM) listened to in several markets.

“Weir decided to manufacture sand wash plants because, like any product, it is important that it comes first from the customer and it is a customer need,” Weir’s vice president of strategy and transformation, Fred Bradner, said.

“We identified the need, and then we also found out there were many products that go into a sand wash plant that we already made.”

Weir designed the Sandmaster range to be portable and easy to assemble, operate, and maintain. This is partly made possible by the quality products Weir produces in-house through its global manufacturing facilities.

The Sandmaster wash plants include well-known parts from Weir, which are produced in-house to the company’s high standards. The Sandmaster sand wash plants also include WARMAN pumps, LINATEX rubber, ENDURON screens, Isogate valves, and CAVEX hydrocyclones.

The CAVEX hydrocyclones are mining-grade hydrocyclones adapted for the sand production industry. According to Weir, the LINATEX rubber lining used in the CAVEX hydrocyclones in Sandmaster plants is four times thicker than conventional linings used by some other producers. It is also included on all of the high-abrasion touchpoints within the machine. This enables customers to reduce their maintenance requirements and face less downtime.

The ENDURON screens have been a long-standing feature of Weir’s portfolio for the quarrying and aggregates industry. The design is well-regarded, and the polyurethane screen media and LINATEX rubber on all the hoses and touchpoints were developed in-house.

A WARMAN pump. Image/Weir

The Sandmaster plants are divided into the SP and DP series, which offer nuanced differences to suit the customer’s approach. Producers can make single-grade sand from the SP series. The SP series excels at removing excess fines or coarse material to deliver a low-moisture product that can be used for stockpiling or conveying. It can also be used to remove unwanted fines and/or clays, convert crusher dust, wash recycled or construction or demolition waste, or recover tailings and grit.

The DP series is capable of producing two separate sand products at the same time, including coarse and fine sand. Raw sand is separated by the split-deck ENDURON dewatering screen, with finer materials passed through into the sump. From there, it is pumped by a WARMAN WGR pump to the CAVEX hydrocyclone, which removes the ultra-fines before it is sent to the ENDURON screen for dewatering and discharged to the stockpile.

The versatility of the Sandmaster sand wash plants has been a key factor with a rise in producers using alternative materials, including crusher dust, to make manufactured sand.

Brewitt said the demand for manufactured sand is occurring in most major global markets.

“Natural sand is running out, so manufactured sand is becoming more and more important,“ he said.

“Crusher dust can be upgraded to manufactured sand with the correct washing, and that wasn’t the sentiment in the beginning.

“I think everyone thought manufactured sand might have been something new they needed to create, but now they’ve realised they just need to upgrade what they already have into a sellable material.

“In the past, it was just sitting there forever, but now, primarily due to legislation and particularly in Europe, local authorities are pushing this along and people are realising that there is quite a lot of sellable sand and aggregate to be made.

“We have to get the sand to a higher specification, a cleaner specification, and to do that, we have to adopt the newer technologies.“

As Brewitt described, some markets have come to rely on the sandscrew technology while others are pivoting to the hydrocyclone-based equipment, like the Sandmaster washplants.

Part of the reason producers are pivoting to the newer technology is the greater recovery rate of cyclone-based technologies. Hydrocyclone systems are better at capturing finer particles, while sand screws are better at dealing with coarse aggregates and changes in feed.

Jarin Wildeman, Weir Regional Sales Leader, NA, showcasing Weir BeltMetrics Gen 2 at AGG-1/World of Asphalt 2025. Image/Guy Woodford

Brewitt told Aggregates Business about how one Weir customer in the US purchased the first Sandmaster unit in the country. Previously, using a sandscrew, they estimated they were losing around 17 to 18 per cent of material during processing, with the losses compounding over time. Since transferring to a 150 tonne per hour (tph) Sandmaster sand wash plant, they have been impressed by its performance and plan to purchase more in the future.

Another customer in Ireland was producing coarse sand with a large amount of waste product. By switching to a Sandmaster sand wash plant, they produced coarse sand and fine sand, which became certified asphalt sand and created a new revenue stream for the business. This customer estimated they saw a return on investment from their Sandmaster unit within the first year of ownership.

“A small amount of capital expenditure on a Sandmaster can pay for itself in 12 to 18 months. The return on investment is absolutely stunning,“ Brewitt said.

“If you could tell your finance manager that you’ll get a return on investment in 12 to 18 months, they’d take the arm off you.“

Weir’s global network supports all of the Sandmaster sand wash plants, which can provide technical service and after-sales support. The company employs over 13,000 people across 60 countries to help its customers.

“The Sandmaster wash plants are supported by a global service network in service centres close to our customers. We have over 150 service centres around the world,“ Bradner said.

Weir BeltMetrics Gen 2

Weir Minerals notes that mine-to-mill optimisation relies on continuously evaluating blasting, crushing, and grinding operations. Monitoring material characteristics on the belt provides key insights into upstream performance, helping to identify issues with crusher throughput and enabling productive adjustments to maximise efficiency and output.

Weir’s AI and stereoscopic imaging-inclusive BeltMetrics Gen 2 belt monitoring solution, showcased at AGG-1/World of Asphalt 2025, is an accurate alternative to sieve analysis that doesn’t interrupt production. Receiving empty belt alerts and particle size data collected with the BeltMetrics system allows users to react quickly to upstream blockages and optimise crusher gap settings to ensure they hit their production goals.

“The biggest thing that our customers like about the solution is that it saves time doing physical belt cuts,“ explains Jarin Wildeman, Weir regional sales leader, North America. “Traditionally, you will have a mining engineer or a geologist taking several different belt cuts [to analyse production activity and maintenance needs]. This means the belt has to stop each time, disrupting production. BeltMetrics Gen 2 enables customers to focus on other areas of their operation.“

Truflo Pumping Systems strengthens after-sales support through strategic

partnership

Olivia Thomson

ITT Blakers and Truflo Pumping Systems have partnered to expand their services across Australia. Image: Image: Truflo Pumping Systems

Truflo Pumping Systems is committed to providing top tier service to its clients, partnering with ITT Blakers in WA to help make a difference.

As mining operations across Australia continue to wrestle with downtime, Truflo Pumping Systems is investing heavily in after-sales support to ensure the downtime its clients experience is kept to a minimum.

A family-owned business with strong roots in Bathurst, Truflo Pumps is expanding its service capabilities across the country to match the reliability of its products.

Recently, Truflo Pumps secured a new alliance with ITT Blakers in Western Australia – an agreement that will be key to achieving its mission of providing top-tier customer service across Australia.

“We manufacture the pumps from start to finish, but what we really want to emphasise now is our repair sector,” Truflo Pumps national operations manager Jason Bemrose told Australian Mining.

“It used to be quite small, but we’re spending a lot of money to build it up so we can provide faster turnaround and stronger customer support.”

Bemrose said the company is placing greater emphasis on repairs, rebuilds and proactive stock holdings, especially in high-demand regions like Queensland and New South Wales.

“Customer support is very important to us,” he said. “To ensure our clients are happy, they need to be serviced quickly, so spending the money and putting the people on the ground is critical to make that happen.”

One of Truflo Pumps’ key initiatives is its investment in wet end stock to enable rapid repair by replacement services.

The company has also launched a successful service exchange program that provides quick replacement of pump components for clients with urgent needs.

“Through our service exchange program, clients send their unit in and receive a replacement unit right away,” Bemrose said. “Sometimes we have it there before they have even removed the old one and that reduces downtime to hours, not weeks.”

This model has resonated particularly well with clients operating in remote locations, where shipping delays can significantly impact production.

“The feedback from those remote sites has been very positive,” Bemrose said. “Some operations simply can’t afford to be down for more than a day or two, so our ability to provide quick turnaround is saving them time and money.”

Truflo Pumps’ partnership with ITT Blakers will expand that same support to WA.

“This is a strategic move to provide faster service and turnaround in WA,” Truflo Pumps’ national sales manager Martin Richardson told Australian Mining.

“ITT is a reputable name in the mining sector and the company is fully equipped to support our customers with rebuilds, overhauls, and stocking key components locally.”

Rather than building a standalone facility which could take years to construct, Truflo Pumps chose to work with an established partner in WA to ensure miners in the area get the same high-quality after-sales experience already available on the East coast.

“For us to establish our own workshop in WA, we’d be looking at a two-to-three-year timeline,” Richardson said. “But through this partnership, we can hit the ground running.”

He says this initiative supports the company’s long-term customer service vision.

“What we gain is customer satisfaction and long-term relationships, and that’s valuable to us.”

Truflo Pumps and ITT Blakers are cross-training staff and aligning systems in their NSW, Queensland and WA service centres to ensure consistency.

Teams from each company will travel between Bathurst and Perth to share knowledge, tools and processes.

“This isn’t just a case of slapping our name on a workshop,” Richardson said. “We’re training each other, investing in the right equipment and making sure we deliver a consistent Truflo Pumps experience.”

From the customer’s perspective, the process is designed to feel seamless, with a dedicated service email address that is monitored by ITT Blakers and Truflo staff to maintain open and timely communication.

“Our goal is for WA customers to feel like they’re working directly with Truflo Pumps,” Richardson said. “They reach out, they get a fast response, and their pump gets back on site quickly.

“It’s about delivering the same level of support no matter where in Australia they are.”

Truflo Pumps’ service exchange model continues to grow, now covering its core wet ends, as well as its Jumbo and Heli-Flo product lines.

With demand increasing for rapid replacement and rebuilds, the company plans to continue investing in stock, systems and people.

“Service exchange for Heli-Flo helical rotor pumps is a hot topic at the moment,” Richardson said. “We’re expanding into that now to keep up with demand.”

At the heart of Truflo Pump’ after-sales expansion is a commitment to reducing downtime and creating long-term value for mining clients.

“We’re not just here to sell a pump,” Richardson said. “We’re here to support our customers through the full life of the equipment and that means fast repairs, smart partnerships and always being ready to respond.” 

This feature appeared in the June 2025 issue of Australian Mining.

Sandvik Mobile Crushing and Screening unveils the QH443E

Sandvik Mobile Crushing

Sandvik Mobile Crushing and Screening is proud to announce the launch of the QH443E. Image: Sandvik

Share on FacebookShare on Twitter

Sandvik Mobile Crushing and Screening is proud to announce the launch of the QH443E, the latest innovation in tracked cone crushers.

This new electric unit has been designed with a focus on sustainability and productivity and is set to revolutionise operations in heavy-duty applications.

The new QH443E is Sandvik’s flagship Q-Range electric-driven cone plant. It takes a significant step towards bridging the gap between tracked mobile, wheeled portable, and stationary plants by combining electric drives and track mobility on a single platform.

The QH443E electric cone crusher completes Sandvik’s revolutionary electric train, which includes the UJ443E fully electric jaw crusher, the QE342e hybrid scalper and the QA452e hybrid triple-deck Doublescreen.

Sustainability at its core

The QH443E features a new and improved heavy duty feeder design and is equipped with electrically driven components. Its advanced design allows for operation through a connection to an external electrical grid supply or on-board generator, providing flexibility and reducing operational costs.

The integration of the latest generation of fuel-efficient engines further enhances flexibility, allowing the unit to be operated via HVO (Hydrotreated Vegetable Oil) or diesel when required, maximizing uptime whilst lowering emissions and operating noise.

Due to the electrification of the onboard components, running the QH443E via the genset can result in up to 25 per cent* fuel savings and a 78 per cent* reduction in hydraulic oil usage compared to previous generations.

Unmatched productivity

The QH443E is designed to maximize uptime and boost output. With the renowned versatility and reliability of the Sandvik CH440 Hydrocone, Constant Liner Performance (CLP), and Hydroset CSS adjustment, this crusher delivers superior power transfer and precision crushing. The new Optik intuitive automation system and My Fleet remote monitoring provide 24/7 fleet management, geo-fencing, and remote operator support, ensure continuous crushing and optimal performance.

One platform, endless possibilities

Engineered to operate in the most hostile environments, the QH443E is ideal for large quarries and mines. Its robust design, featuring a unibody mainframe and premium components, ensures durability and strength. The load-sensing system for the feeder drive, camera, and level sensor guarantees continuous crushing, while the choice of chambers, throws, and settings allows for customization to suit a wide range of applications.

Safety and Support

Safety is paramount in the design of the QH443E. The unit includes remote camera viewing of the crushing chamber, 270° access around the crusher for easy maintenance, and mandatory audible and visual warnings for safe operation. Our extensive global distributor and sales support network ensures that you receive the best support for your operations.

The Sandvik QH443E represents a significant step forward in the evolution of tracked cone crushers. With its focus on electrification, sustainability, and productivity, it is the perfect solution for large quarries and mines looking to enhance their operations. Experience the future of crushing with the Sandvik QH443E.

Tags: Crushing Static & Mobile

Metso expands Nordberg HPe crusher series

by Adam Daunt

Metso Hpe

Metso has released the HP450e. Image: Metso

Share on FacebookShare on Twitter

Metso has continued to push the boundaries of its Nordberg HPe crusher series through another expansion of the crushing range.

The HPe range was introduced by Metso in 2023 and in just two years, has grown to six models which encompass crushing solutions from secondary to tertiary and quaternary crushing.

The HPe is an evolution of the Nordberg HP cone crusher technology. Since being released by Metso has seen more than 200 units sold globally while old HP models have been retrofitted with HPe upgrade kits.

“With the latest addition of the Nordberg HPe crusher series, we are able to offer customers the ideal balance of power and efficiency for their specific crushing needs,” Metso HP cones product manager Ilkka Somero said.

“The HP450e, as a mid-range unit, is designed for customers who require reliable, high-capacity crushing without excessive energy consumption.

“With this unit, we have further improved its application flexibility so that customers get the maximum production and yield of wanted end products.”

Metso showcased the sixth model of the HPe series, the HP450e, at bauma 2025 in Munich, Germany. Attendees to the trade show were able to witness a launch event for the HP450e.

According to Metso, the HP450e has 10 per cent more head motion, 13 per cent more power and 20 per cent more force than its predecessor model. The new chamber design makes it more efficient while the head spin brake enables higher uptime and it is a more environmentally friendly solution due to backing material not being required.

Somero said the market response to the new HPe models highlights a clear industry shift toward higher efficiency, safety and sustainability in crushing operations.

Metso offers upgrade options for customers with earlier generation HP crushers. Many of the new HPe features can be applied to existing units through upgrades, including no-backing liners that reduce maintenance downtime, a redesigned split nut for improved safety and easier maintenance, and a crusher head spin brake that extends liner life.

Additionally, most spare and wear parts from the HPe series are compatible with HP crushers, providing cost-effective and operational benefits for mixed fleets.

With these six HPe crushers, a wide range of 10 different chamber profiles, advanced simulation software, and Metso’s expertise, customers can optimise their operations and achieve their production targets. Designed for versatility, Metso’s HPe crushers can be configured for various applications, from wheel-mounted Nordwheeler setups to modular Nordplant installations and track-mounted Lokotrack units.

ROTO Pumps delivers mine site system overhaul

by Kelsie Tibben

ROTO’s bespoke dual-positive displacement helical rotor pump. Image: ROTO Pumps

ROTO’s bespoke dual-positive displacement helical rotor pump. Image: ROTO Pumps

Share on FacebookShare on Twitter

ROTO Pumps recently helped a mining client out of a sticky situation.

Having supplied solutions to the mining industry since 1968, ROTO Pumps was an obvious call for one miner with serious pumping woes.

The mine’s entire processing and dewatering network was struggling to keep up with the demands of the site, with significant implications for overall operations. The project deals with harsh conditions and aggressive media that requires a high head pressure, calling for pumps that are capable of heavy lifting beyond the norm.

ROTO Queensland and Northern Territory manager Brett Layt said the team deployed to site immediately and met the challenge head-on.

“ROTO has capabilities to supply any PCP [progressing cavity pump] package worldwide, meeting any site or national standards and requirements,” Layt told Mining.

“For this client, we created a bespoke dual-positive displacement helical rotor pump package with in-built dewatering fish tank to meet and exceed the site-specific application.”

The solution was swiftly implemented at the mine site by a team of ROTO pumping experts.

How did they deliver so quickly?

“We hold stock of all required mining pump service parts ready to go,” Layt said.

“Our knowledgeable team are always on hand to troubleshoot any enquires sent our way.

“Our optioned package for this client is designed to increase the service life of the pump, with multiple baffles and flushing points to mitigate the harshness of the media collected in the fish tank.”

ROTO also offers on-site after-sales training on its pumps and systems to help ensure its clients get the most out of their solutions.

For Layt, keeping the mining industry’s pumping systems running smoothly is about more than just a job well done.

“Our adaptability and attention to detail for the requirements of every application really set us apart,” he said.

“We strive to not only be a cost-effective option but also smash lead time while providing a more personable experience.”

Over more than 57 years spent gaining insights into the mining industry’s major pumping challenges, ROTO has developed a comprehensive range of progressive cavity pumps and systems to effectively handle all mining and explosive applications.

Central to the company’s practices is a deep commitment to, and passion for, supporting clients to set and achieve larger goals than ever before. Layt believes this is the only way to drive the industry forward into a successful future.

“ROTO’s range and capabilities are forever growing and evolving,” he said. “We will continue to be a valued ally with our customers to provide stress-free pumping solutions.”

This feature also appears in the Autumn issue of Mining.

Metso showcases their HP350e crusher

by Adam Daunt

Metso HPE

The HP350e is a new innovation from Metso. Image: Metso

Share on FacebookShare on Twitter

Metso has pushed ahead with a new evolution of its HP range, introducing the HP350e and other models for crushing operators.


How do you evolve a recognised brand to become even better?

That question challenged Metso as it sought to develop the Nordberg HP, which was reviewing the classic workhorse from the “ground up.” The result is the Nordberg HPe.

The Nordberg HPe series aims to provide improved performance, uptime, application coverage, and serviceability more sustainably than its predecessor.

“Nordberg HP cone crushers are globally accepted as the go-to crusher for aggregates and mining,” Metso’s cone crusher product range Ilkka Somero said.

“The range continues to evolve and align with customer and industry needs and demands. Today there are drivers pushing for ever higher efficiency in productivity. In terms of overall production but also in terms of production of most valuable product fractions.

“In HPe development, this is achieved with higher overall performance, higher uptime with ease of service and maintenance as well as with enhanced application flexibility.”

When Metso examined the key mining and aggregates industries it serves worldwide, it noticed efficiency is the central focus of many operations. Quarry and mining businesses are looking to achieve maximum performance in throughput, reduction, or higher yield of certain aggregate fractions.

The new Nordberg HPe series needed to meet all of these requirements while also addressing the sustainability challenges that many businesses face every day.

Metso has further developed the kinematical crushing action and crusher chamber. The improvements balance kinematics, chambers, release force, and power rating. The redesign enables the HPe series to deliver more head motion, higher power, and new chambers. The upgrades of the kinetics enable the Nordberg HPe series to cover more applications than previous models.

Operators will have alternative kinetics along with improved chamber designs and application-specific options to select from. Metso’s team can assist customers in creating the optimal chamber for their needs.

According to Metso’s data, the new HP350e crusher delivers ten per cent performance compared to the traditional HP300 crusher in secondary or tertiary applications.

“Our development engineers and manufacturing facilities have provided a full range of eRange cones from 200 to 900kW, following a full redesign of a classic workhorse. We are excited to bring these products to the market to increase our customer’s bottom line,” Metso’s business development manager for aggregates, John O’Reilly, said.

“The evolution enables us to meet industry needs where you want more production and, more importantly, more efficiency when producing the needed product yields.”

One of the major upgrades in the HPe series involves the crusher liners. Metso’s latest update allows for the installation of these liners without backing material. While this may seem minor, the update significantly simplifies liner changes, making them easier and safer for operators.

Metso will feature the HPe range at international trade shows throughout 2025. Image: Metso

This reduces the need for quarries to source, store and transport backing compounds. Operators will also not need to handle, mix and pour the backing material, making operations safer and line change-outs faster. Metso can also tailor the liners to suit particular applications, including manufactured sand or specific aggregate fractions with its NF liner.

The anti-spin brake and ring bounce monitoring feature help extend the lifespan of the liners while also safeguarding the machine.

These upgrades will help operators increase machine uptime and productivity in the quarry. Metso has designed the HPe range, including the HP350e, to fit within the HP300 footprint while delivering more power.

“It is an evolution, but it is not just that we’ve put more power onto the machine and redesigned the cavity kinematics; there are more safety features, which is very important and simpler maintenance,” O’Reilly said. 

“It has the same footprint as its predecessors. For example, the HP450e replaces the existing HP400 but is the same size on the outside.  Because it is the same size envelope, there is no extra structural work to replace it. You can switch one in and one out.” 

The HPe series is set to be unveiled progressively throughout the year by Metso at the world’s biggest quarrying trade shows.

The original equipment manufacturer is set to launch the HP450e at AGG-1 in St Louis. Attendees to bauma 2025 in Munich, Germany, can witness the debut of the HP600e. Other launches with the Nordberg HPe range will include the 600e later in 2025.

Metso’s Australian team and service and support network will fully support the introduction of the HPe series into Australia. With extensive industry experience, the team can help optimise a Nordberg HPe series crusher to suit the customer’s application.

“Metso is strongly focused on supporting the Australian quarry industry with world-class aggregate-producing solutions. The Nordberg HPe range is the evolution we believe our customers have been asking for,” O’Reilly said. •